Casting vs Forging vs CNC: How to Choose the Right Process
Choosing the wrong manufacturing process can double your cost, delay delivery, or fail in service. This guide gives engineers and buyers a practical decision framework based on geometry, material, quantity, tolerance and application.
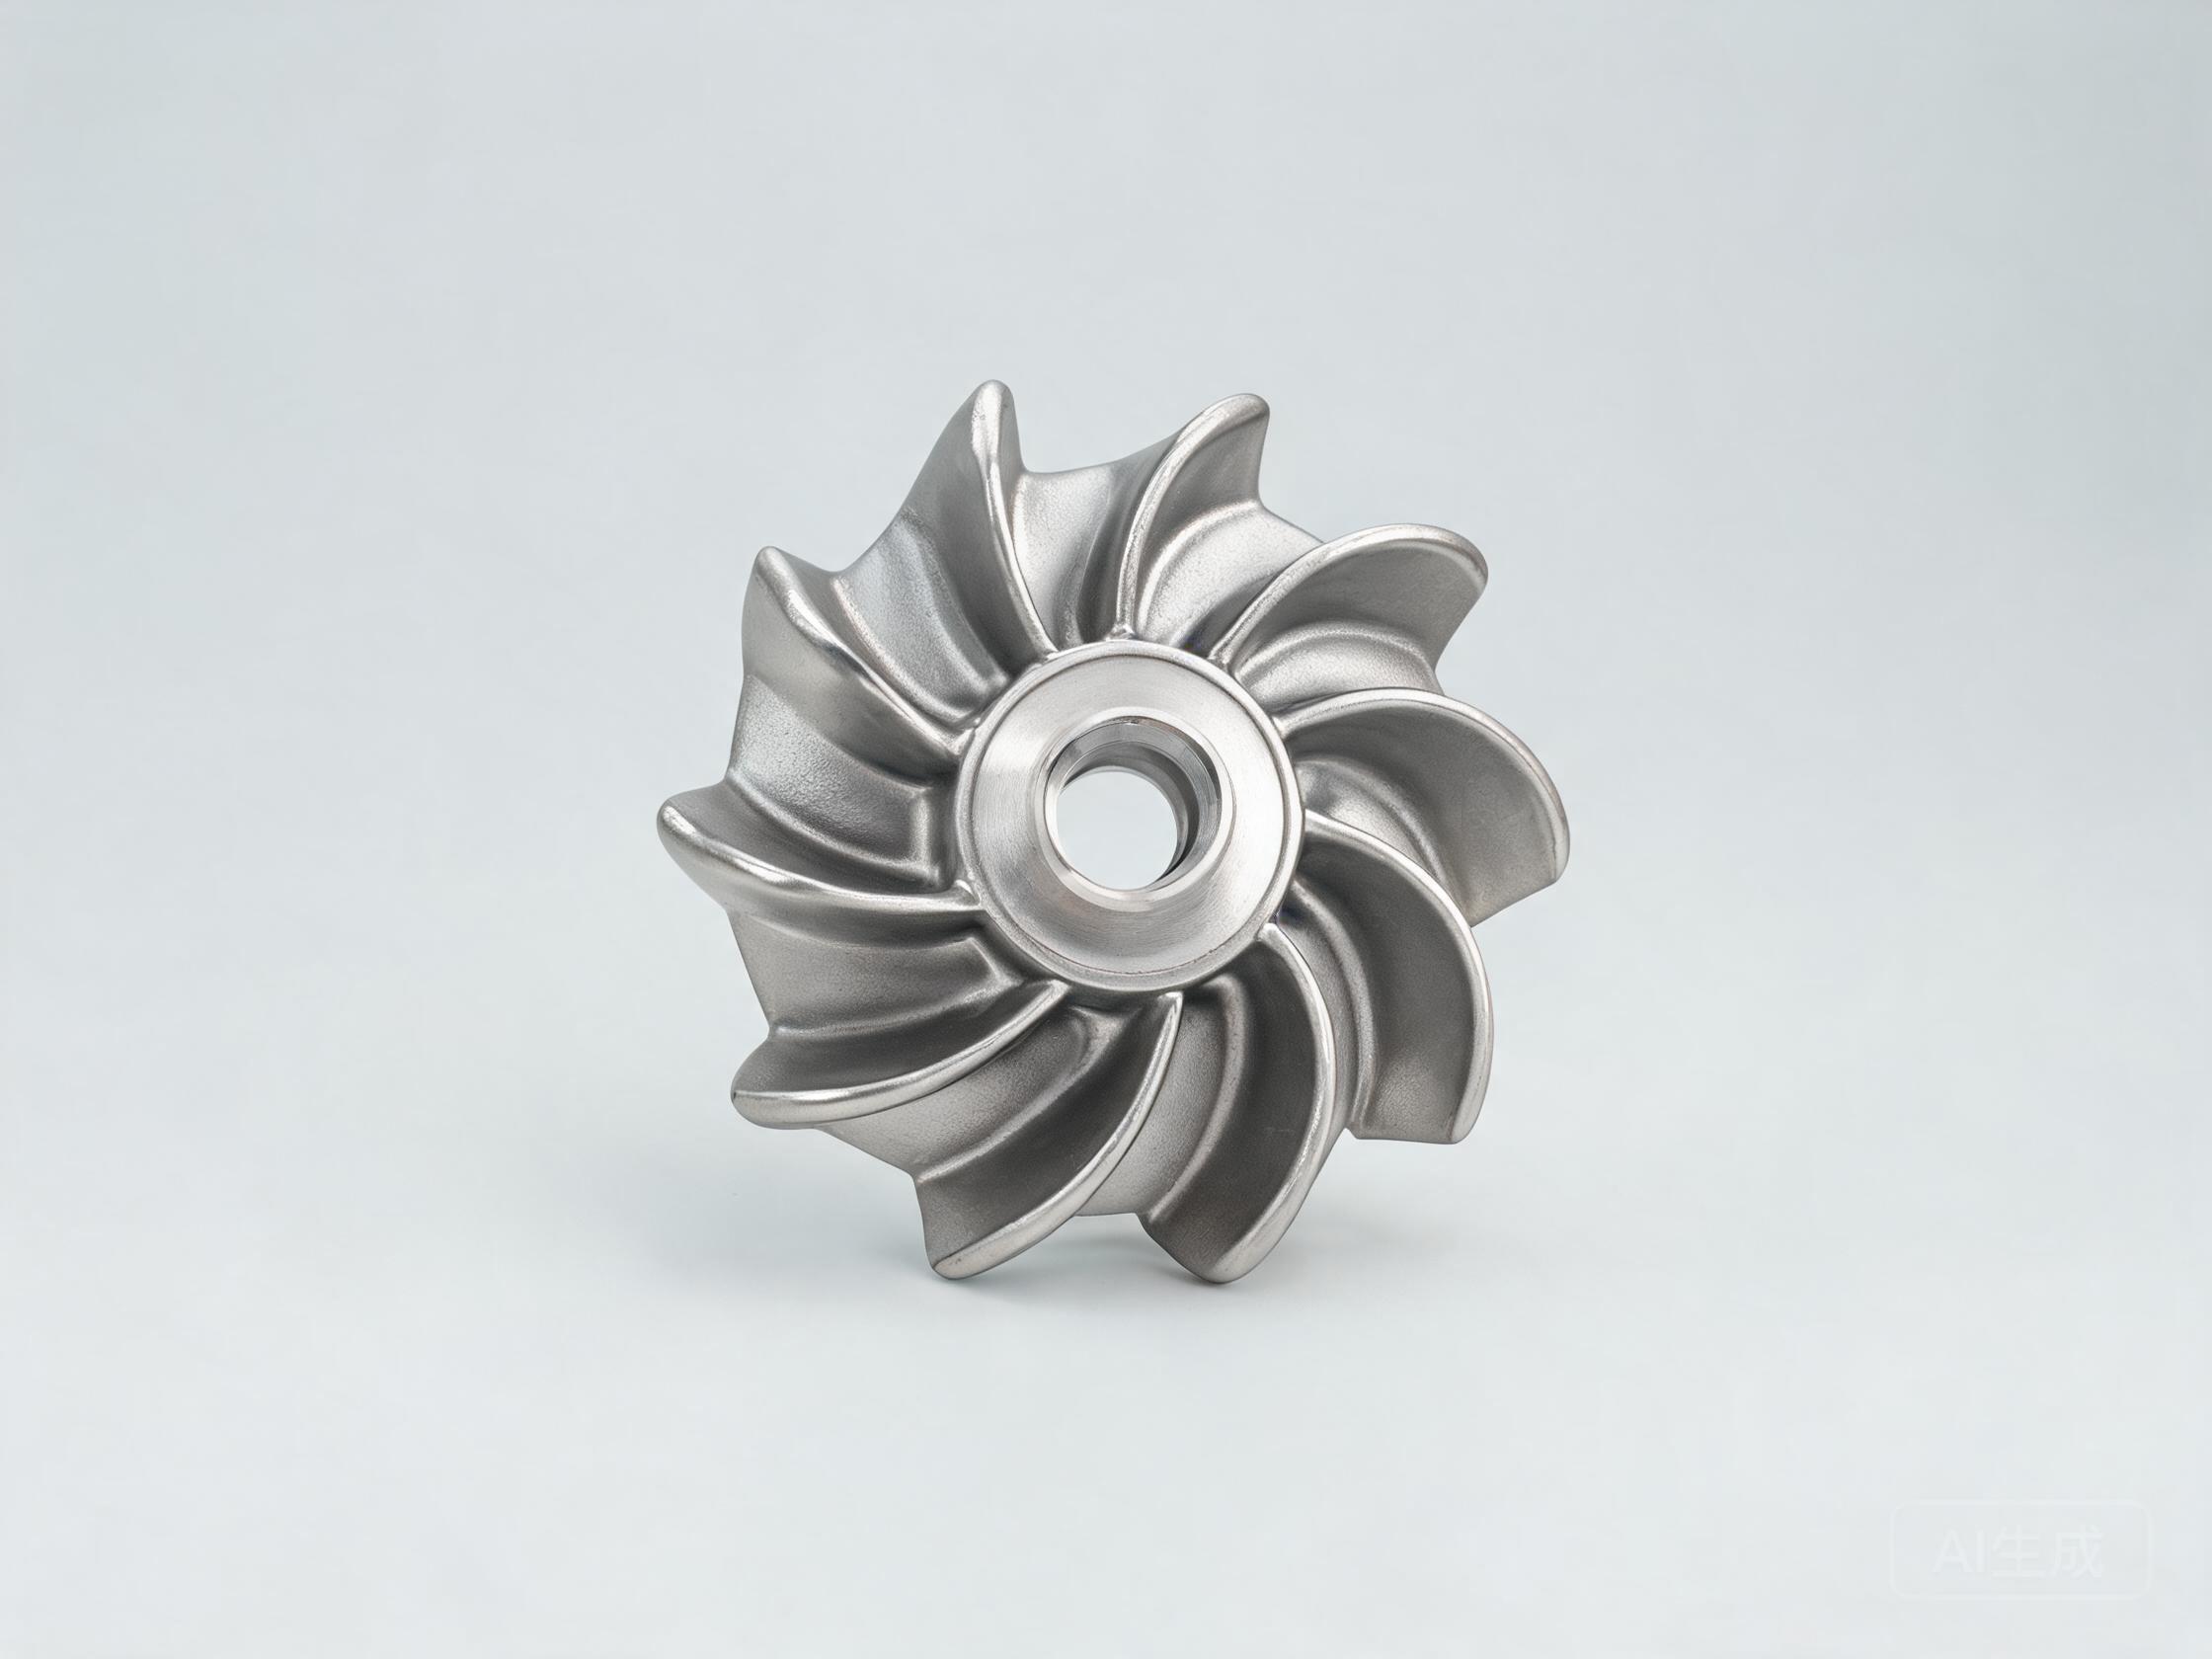
Disclosure: we manufacture castings, forgings and CNC-machined parts. This guide is written to help you choose the right process — even if that process isn't the one we'd most profit from. A good supplier tells you the truth.
Why Process Choice Matters
The three core processes — casting, forging and CNC machining — each handle different geometries, materials, quantities and quality requirements. The "right" answer is rarely universal; it depends on your specific part.
Three common mistakes we see:
- The wrong process — e.g. machining a part from solid when casting would cut cost by half.
- The wrong supplier — the lowest quote often means the highest total cost.
- The wrong cost target — tooling, material utilization and volume all change the final price.
The Decision Framework
Work through these five questions in order.
1. What geometry? (Shape complexity)
| Condition | Best fit | Why |
|---|---|---|
| Complex internal cavities, thin walls, 3D forms | Casting | Molten metal fills complex shapes; casting simulates and produces hollow or intricate forms. |
| Simple, solid, high-strength shapes | Forging | Refined grain flow gives superior strength and fatigue life. |
| Precise, boxy or CNC-friendly features (holes, threads, slots) | CNC | Machining removes material to reach tight tolerances and detailed features. |
2. What material?
- Casting handles a very wide range — stainless steel, carbon steel, alloy steel, ductile iron, nickel/cobalt alloys, non-ferrous.
- Forging is common for carbon/alloy steels, stainless, aluminum, copper alloys.
- CNC can machine nearly any material on a blank, but is often least economical for very hard or very large volumes.
Rule of thumb on volume
Prototype / low volume (1–50 pcs): CNC machining from a blank, or rapid prototyping.
Production (100s–1000s): casting or forging, because tooling cost is amortized and per-part cost drops sharply.
3. What quantity?
| Quantity | Recommended | Reason |
|---|---|---|
| 1–50 | CNC / rapid prototype | No tooling cost; fast turnaround for samples and testing. |
| 50–500 | Evaluate both | Compare tooling amortization vs machining time. |
| 500+ | Casting / forging | Per-part material use and efficiency favor closed-die forming. |
4. What tolerance and surface?
- Tightest tolerances & features: CNC machining (e.g. GB/T 1800.1 grade 5–7 linear).
- Good net-shape: investment casting (e.g. ISO 8062 DCTG4-6) with surface ≤ Ra6.3, down to Ra3.2 after treatment.
- Fits and final accuracy: almost always finished with machining after casting/forging.
In practice, the best result is often a combination: cast or forge the near-net shape, then CNC-machine the critical surfaces and threads.
5. What is the total cost?
- Tooling: casting/forging require dies or patterns (one-time). CNC needs no tooling, just per-hour cost.
- Material utilization: casting/forging waste less material than machining from a solid block.
- Lead time: for a first sample, CNC is fastest; for ongoing production, forming is faster per part.
Choose Casting when
Complex geometry, internal cavities, ductile/brittle-capable materials, medium-to-high volume, structural or flow-control parts like valve bodies and pump bodies.
Choose Forging when
You need maximum strength, impact resistance and fatigue life in a simple to moderately complex shape, and volume justifies tooling.
Choose CNC when
You need tight tolerances, detailed features, low quantity, or a prototype — or as a finishing step after casting/forging.
Combine them when
Form near-net shape, then machine critical surfaces. This is often the lowest-cost path to a quality part at volume.
A Practical Example: Valve Body
A stainless valve body with internal flow passages and threaded connections. Machining the whole thing from solid would waste a huge amount of expensive material. Casting the hollow body (investment casting) dramatically cuts material, then CNC machines the flange faces and threads for a sealed fit — a classic cast + machine combination.
Not sure which process fits your part?
Send your drawing. We'll return a technical review with the recommended process, expected tolerance and a transparent quote.
Start a Project →← Back to Blog · Related: Forging & Heat Treatment · CNC Machining Tolerances Explained · How Investment Casting Works · Our Forging Capability