What Is Investment Casting? Process, Materials & When to Use It
Investment casting — also known as lost-wax casting — is one of the oldest and most precise metal-forming processes. This guide explains how it works, what materials it supports, and how to decide if it is right for your part.
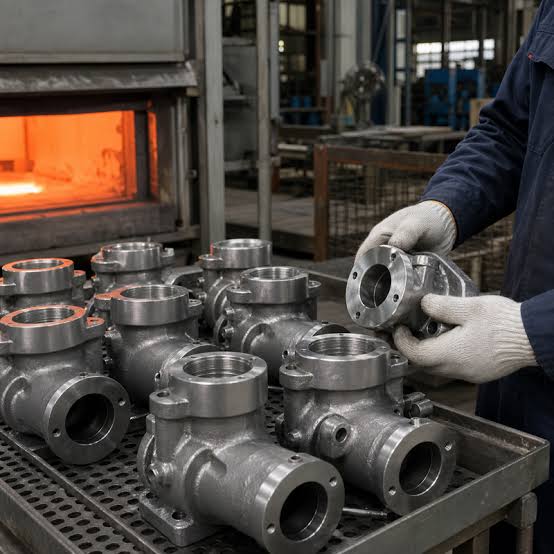
TL;DR — Key Takeaways
- Investment casting uses a wax pattern inside a ceramic shell; the wax is melted out and replaced by molten metal.
- Best for complex geometries, thin walls, tight tolerances (±0.05 mm/25 mm), and excellent surface finish (Ra 1.6–6.3 μm).
- Materials: carbon steel, alloy steel, stainless steel, aluminum, copper, nickel superalloys.
- More expensive per piece than sand casting, but eliminates machining on complex features.
- Economical for volumes of 500+ pieces; tooling takes 3–5 weeks, samples 2–3 weeks.
1. What Is Investment Casting?
Investment casting is a precision manufacturing process that creates metal parts by pouring molten metal into a ceramic mold. The mold is built around a disposable wax pattern — hence the alternative name "lost-wax casting." The wax is "lost" (melted and drained) before the metal is poured, leaving a cavity that exactly mirrors the desired part shape.
The process dates back over 5,000 years to ancient Mesopotamia and Egypt, where it was used for jewelry and religious artifacts. Today it is a cornerstone of modern industrial manufacturing, used in aerospace, automotive, energy, medical, and general engineering.
2. How the Investment Casting Process Works
The process consists of seven core steps. Each step directly affects the final part quality, so understanding them helps you write better specifications and audit suppliers effectively.
1Pattern Making (Wax Injection)
A steel or aluminum injection die is machined to the negative shape of the part. Molten wax is injected under pressure into the die cavity, creating an exact wax replica of the final part. Multiple wax patterns are typically assembled onto a central "sprue" to form a "tree" that will feed molten metal to several parts at once.
2Shell Building (Investing)
The wax tree is repeatedly dipped into a ceramic slurry (usually colloidal silica or ethyl silicate binder with refractory flour) and then coated with refractory sand. This is repeated 5–9 times to build up a rigid ceramic shell 8–12 mm thick. The first "prime coat" determines surface quality; subsequent "backup coats" provide structural strength.
3Dewaxing
The ceramic shell with wax inside is heated in a steam autoclave or flash-fire furnace. The wax melts and drains out (and is typically recovered and reused). The shell is now a hollow negative of the part — the "investment" mold.
4Preheating & Pouring
The empty shell is preheated to 800–1100°C to remove residual moisture, burn out any wax residue, and improve metal flow. Molten metal is then poured — usually by gravity, though vacuum or centrifugal pouring is used for reactive alloys like titanium or to reduce porosity.
5Solidification & Shell Removal
After the metal solidifies and cools, the ceramic shell is mechanically broken (vibration, hammering, or sandblasting) to free the castings. The parts are then cut from the sprue tree.
6Finishing & Heat Treatment
Gates and risers are ground off. Castings may undergo heat treatment (solution annealing, quenching, tempering) to achieve the required mechanical properties. Shot blasting or polishing improves surface finish. Critical surfaces may require secondary CNC machining.
7Inspection
Final inspection includes dimensional checks (CMM, gauges), material verification (spectrometer, PMI), visual inspection, surface finish measurement, and — depending on the application — NDT such as penetrant (PT), radiographic (RT), or ultrasonic (UT) testing.
3. Materials for Investment Casting
Investment casting is compatible with virtually any castable metal. The table below summarizes the most common material groups and their typical applications.
| Material Group | Common Grades | Typical Applications |
|---|---|---|
| Carbon Steel | WCB, 1030, 1045 | Valves, pumps, structural brackets |
| Alloy Steel | 4130, 4140, 4340, 8620 | Gears, shafts, automotive components |
| Stainless Steel | CF8 (304), CF8M (316), CF3M (316L), 17-4PH | Food/medical equipment, marine, aerospace |
| Tool Steel | H13, P20, D2 | Dies, molds, cutting tools |
| Aluminum | A356, A357, 319, 355 | Aerospace housings, heat sinks |
| Copper Alloys | C83600, C95400, C95800 | Bearings, bushings, marine hardware |
| Nickel Superalloys | Inconel 718, 625, Hastelloy X | Gas turbine blades, aerospace hot sections |
4. Tolerances & Surface Finish
Investment casting is chosen primarily for its precision. As-cast capabilities are far superior to sand casting, though not as tight as CNC machining.
Linear Tolerance
±0.05 mm per 25 mm (±0.002 in/in) for general dimensions. Critical features can be held to ±0.025 mm with tighter process control.
Surface Finish
As-cast: Ra 1.6–6.3 μm (63–250 μin). After shot blast: Ra 3.2–12.5 μm. After machining/polishing: Ra 0.4–0.8 μm.
Minimum Wall Thickness
~1.0–1.5 mm for small parts, ~2.0–2.5 mm for larger parts. Thinner walls than sand casting.
Draft Angle
0.5°–1° minimum (often zero draft possible on small features). Sand casting needs 1°–3°.
5. Investment Casting vs Sand Casting vs CNC Machining
Choosing the right process is the first and most important decision in any metal part sourcing project. Here is how the three main options compare:
| Factor | Investment Casting | Sand Casting | CNC Machining |
|---|---|---|---|
| Complexity | Excellent (internal passages, thin walls) | Good | Limited (no undercuts) |
| Tolerance | ±0.05 mm/25 mm | ±0.25 mm/25 mm | ±0.005 mm |
| Surface Finish | Ra 1.6–6.3 μm | Ra 6.3–12.5 μm | Ra 0.4–3.2 μm |
| Tooling Cost | Medium ($3k–$15k) | Low-Medium | Low (no tooling) |
| Unit Cost | Medium-High | Low | High (material waste) |
| Minimum Volume | ~100 pcs | ~10 pcs | 1 pc |
| Max Part Size | ~100 kg | ~10,000+ kg | Limited by machine |
Rule of Thumb
If your part has complex geometry, thin walls, or internal features that would require extensive CNC machining — and you need 500+ pieces per year — investment casting is usually the most cost-effective choice. For large, simple parts, sand casting wins. For low volumes or very tight tolerances, CNC from solid bar or plate may be better.
6. When NOT to Use Investment Casting
Investment casting is not always the best choice. Avoid it when:
- Your part is very large (over ~100 kg or 500 mm in any dimension) — tooling and shell costs become prohibitive.
- You need only 1–50 pieces — the tooling cost cannot be amortized.
- Your part is a simple shape that can be CNC machined from bar stock with low material waste.
- You require tolerances tighter than ±0.025 mm — investment casting alone cannot achieve this without secondary machining.
7. Cost Drivers in Investment Casting
When requesting quotes, understanding cost drivers helps you design parts that are cheaper to produce without compromising function.
- Part complexity and weight — More wax, more ceramic, more metal, longer cycle time.
- Material grade — Stainless steel and superalloys cost more than carbon steel; scrap rates vary.
- Tolerance and finish requirements — Tighter specs mean higher reject rates and more secondary machining.
- Annual volume — Higher volume amortizes tooling and reduces per-piece cost.
- Inspection and NDT scope — Full RT/UT inspection adds significant cost.
8. Sourcing Investment Castings From China
China is the world's largest investment casting producer, with thousands of foundries ranging from small shops to aerospace-qualified facilities. Sourcing from China offers 30–60% cost savings vs. Western foundries, but requires careful supplier selection and quality control.
The most common mistakes buyers make when sourcing castings from China include:
- Choosing the supplier purely on price, without auditing their process capability.
- Sending incomplete drawings or specifications, leading to different suppliers quoting different scopes.
- Skipping pre-shipment inspection, only to discover defects after the goods arrive.
- Not clarifying material traceability and heat treatment requirements upfront.
How GRDH Precision Helps
We act as your technical buyer on the ground in China: we audit foundries by equipment, certifications, and similar-part experience; compare quotes on an apples-to-apples basis; follow up production milestones; coordinate pre-shipment inspection; and manage logistics. You get one point of contact and lower risk — without the overhead of running your own China office.
How to Source Investment Castings From China — Complete Guide." data-zh="关于如何从中国采购熔模铸件的完整分步指南,请参阅我们的专题文章:如何从中国采购熔模铸件——完整指南。">For a complete step-by-step guide on how to source investment castings from China, see our dedicated article: How to Source Investment Castings From China — Complete Guide.
9. Conclusion
Investment casting is a versatile precision process that shines when you need complex geometry, thin walls, good surface finish, and tight tolerances in medium-to-high volumes. Its higher tooling and per-piece cost vs. sand casting is often offset by savings in secondary machining and assembly.
The key to success is choosing the right process for your part — and the right supplier to execute it. If you are unsure whether investment casting is right for your application, send us your drawing and we will recommend the most cost-effective manufacturing route.
Not Sure Which Process Fits Your Part?
Send us your drawing and we will recommend the right manufacturing process — casting, forging, or CNC machining — from qualified Chinese suppliers.
Start a Project →